Reliable Vacuum Conveying Solutions

Manufactured from polished acid-resistant stainless steel (304 or 316 grade), VMECA’s reliable vacuum conveying solutions provide hygienic, low-maintenance answer for industries where product quality and cleanliness are paramount.

Every application is assessed by Simmatic’s experienced engineers to ensure the most suitable conveying solution for your process. Whether you’re handling food ingredients, pharmaceutical powders, chemicals, plastics or other free-flowing materials, Simmatic can help you specify the right system for your production requirements. Take a look at the complete range of VMECA VTC Vacuum Conveyors – high-performance pneumatic conveying systems designed to transport powders, granules and other dry bulk materials safely, efficiently and without dust.

Vacuum Conveying Dry Materials

The VMECA VTC range

Vacuum Conveyors use compressed air to generate a powerful vacuum, allowing dry materials to be transferred through enclosed pipework without mechanical conveying equipment.

This vacuum conveying method offers numerous advantages over conventional screw or belt conveyors, including cleaner operation, reduced maintenance and greater flexibility when integrating into existing production lines.

Available with automatic filter cleaning systems and optional ATEX certification, the VTC range is ideal for hygienic production environments and hazardous dust applications.

Reliable Vacuum Conveying Solutions:

  • Dust-free transfer of powders, granules and dry bulk materials
  • Hygienic stainless steel construction (304 or 316 grade)
  • Low operating noise (typically 68–76 dB)
  • Energy-efficient compressed air operation
  • Minimal maintenance with no moving mechanical conveying parts
  • Automatic filter cleaning options available
  • ATEX-approved models for explosive dust atmospheres
  • Compact design for easy integration into existing production facilities
  • Suitable for food, pharmaceutical, chemical, plastics and other industrial applications
  • VMECA Vacuum Conveyors Systems supported by Simmatic

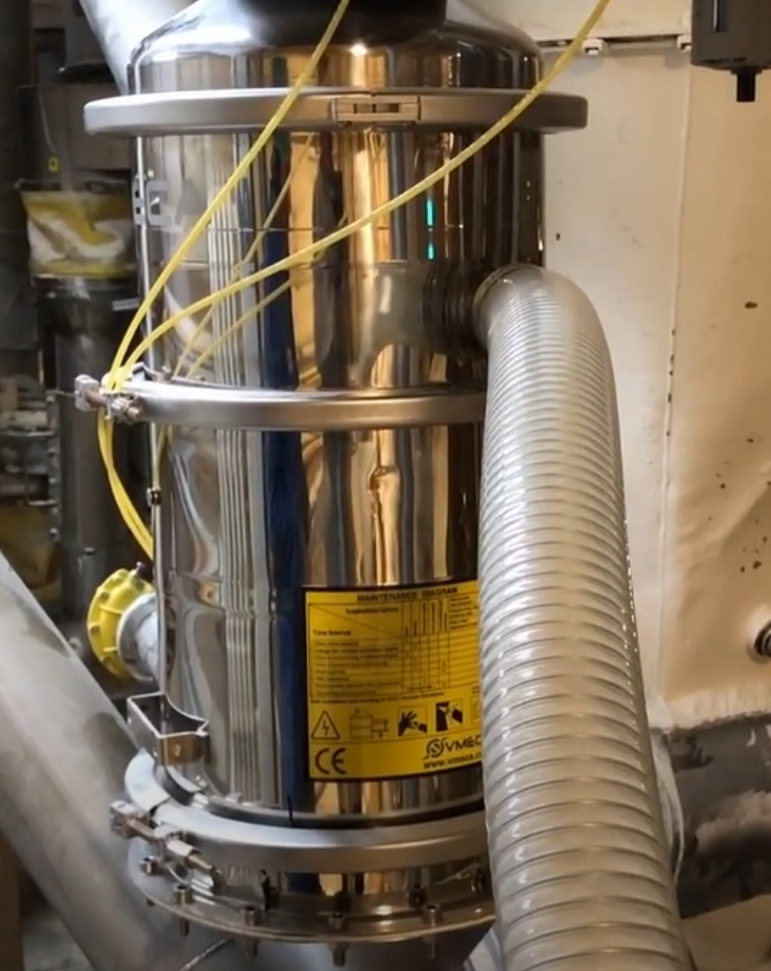
Pictured right is the VTC200 

Model:     VTC200
Capacity (tph):     1.5 ton/hour
Air Consumption @ 6 bar (Nl/min):     832Nl/min
Noise Level:     68-76

VMECA VTC Vacuum Conveyor Range…

Reliable vacuum conveying

Maximum Capacity

0.9 tonnes/hour

2.2 tonnes/hour

5.5 tonnes/hour

8.5 tonnes/hour

Air Consumption @ 6 bar

416 Nl/min

1,600 Nl/min

3,360 Nl/min

4,920 Nl/min

Noise Level

68–76 dB

68–76 dB

68–76 dB

68–76 dB

From compact systems handling less than one tonne per hour to high-capacity conveyors capable of transferring over eight tonnes per hour, there’s a VTC model to suit virtually any production requirement.

How do VMECA Vacuum Conveyors Work?

VMECA VTC conveyors utilise a multi-stage compressed air vacuum pump to create negative pressure within the conveying line. Atmospheric pressure then gently draws product through the enclosed pipework and into the receiver.

Vacuum Conveyor

VTC Vacuum Conveyor

Because there are no moving mechanical components in contact with the product, vacuum conveying provides a gentle, hygienic and contamination-free method of transferring materials while significantly reducing dust emissions.

Applications & Real-World Use

  • Ideal for industries like foodpharmaceuticalschemicals, and plastics, where cleanliness and product integrity are critical.
  • ATEX-certified versions accommodate hazardous environmentsrequiring explosion-safe equipment.
  • Simmatic offers support to tailor systems to specific use cases – even handling tricky applications

VMECA’s reliable vacuum conveying solutions are often complimented for solving complex space and handling challenges, efficiently replacing traditional conveyors with overhead, dust-controlling alternatives.

Why Choose Simmatic?

Selecting the correct vacuum conveying system requires more than simply matching a capacity figure. At Simmatic, our engineers evaluate every application, considering product characteristics, conveying distance, throughput, hygiene requirements and available utilities before recommending the most appropriate solution. Our services include:

  • Application assessment
  • Product testing
  • System design
  • ATEX guidance
  • Control system integration
  • Installation support
  • Ongoing technical assistance

Whether you’re upgrading an existing production line or designing a new process, we’ll help you achieve reliable, efficient and hygienic material handling.

Watch VMECA Vacuum Conveyors in Action….

Speak to the Vacuum Conveying Specialists

Our team can advise on throughput calculations, ATEX requirements, pipework sizing, filtration options and control systems to deliver a vacuum conveying solution tailored to your production process. Contact Simmatic today to discuss your application or request a quotation.